Developing and supplying quality pharmaceutical ingredients with a focus on consistent standards, reliable processes and long-term partnerships.
Pharmaceutical development to manufacturing, we follow controlled processes and quality practices to meet the changing needs of the industry.
We are leading manufactures of Oxetacaine, Mephentermine sulphate, Carbimazole, Methimazole, Nitazoxanide, Nitrofurantoin, Nitrofurazone, Rosuvastatin and Perindopril, with annual capacity of 150 MT. All products are manufactured using state of art technology with highest quality in WHO-GMP certified facility.
Ceramic foundry filters and refractories, manufactured under strict process controls.
Pipe Line API components are manufactured for reliable performance in demanding pipeline applications. Designed with precision and consistency, they support smooth operation, durability, and dependable service across various industrial requirements.
View more
Commercial API components are manufactured to meet diverse industrial and commercial requirements. With precise dimensions, consistent quality, and reliable performance, they are suitable for applications where durability and dependable functionality are essential.
View more
Intermediates are manufactured with accurate dimensions and consistent quality for use in various industrial applications. They are designed to provide reliable performance, dimensional stability, and suitability for different processing and assembly requirements.
View moreLivmore Life Sciences combines focused API manufacturing, quality systems and technical expertise to deliver consistent pharmaceutical ingredients for diverse market requirements.
Focused on the development and manufacturing of Active Pharmaceutical Ingredients with controlled processes and technical expertise.
Well-equipped manufacturing facilities support controlled production, process consistency and dependable supply.
Quality is maintained through defined processes, testing and systematic controls across manufacturing activities.
Continuous process development and technical improvement support new products and evolving pharmaceutical requirements.
Since 2016, Livmore Life Sciences has been focused on the development and manufacturing of Active Pharmaceutical Ingredients, advanced intermediates and specialty chemicals.
Annual Manufacturing Capacity (MT)
Installed Reaction Capacity
Commercial API Products
Quality Commitment
Total Facility Area (Sq. M.)
Livmore Life Sciences supplies APIs and advanced intermediates to pharmaceutical markets, supporting customers with consistent quality, reliable manufacturing and responsive service.
Equipped with modern technology, precision manufacturing, and world-class qualitysystems to deliver trusted pharmaceutical solutions.
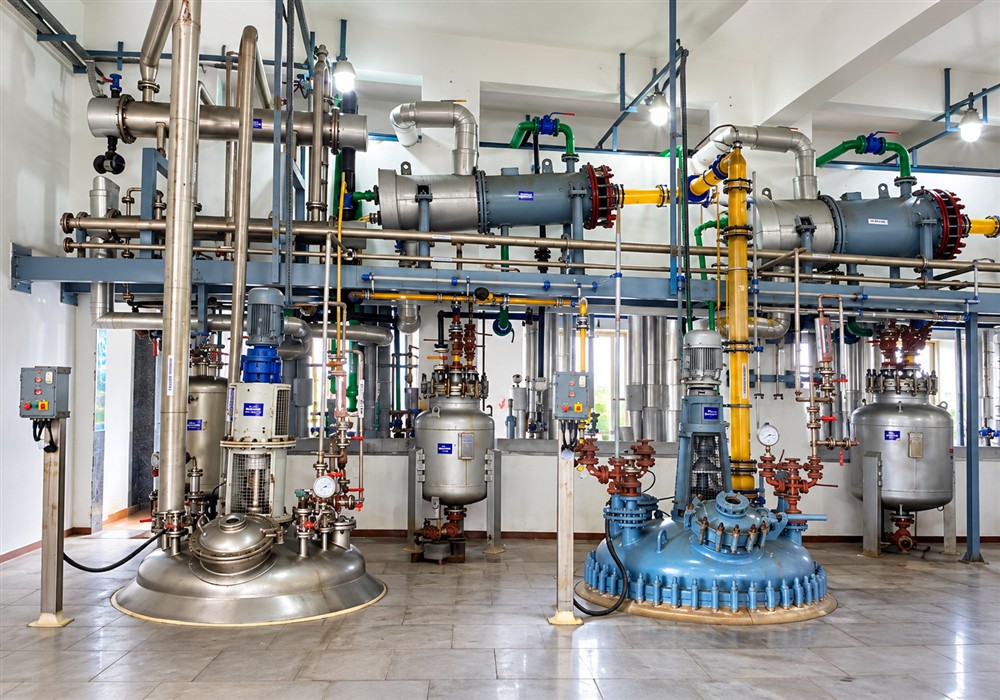
Controlled API manufacturing facilities with reactor systems, process areas and infrastructure for steady production needs.
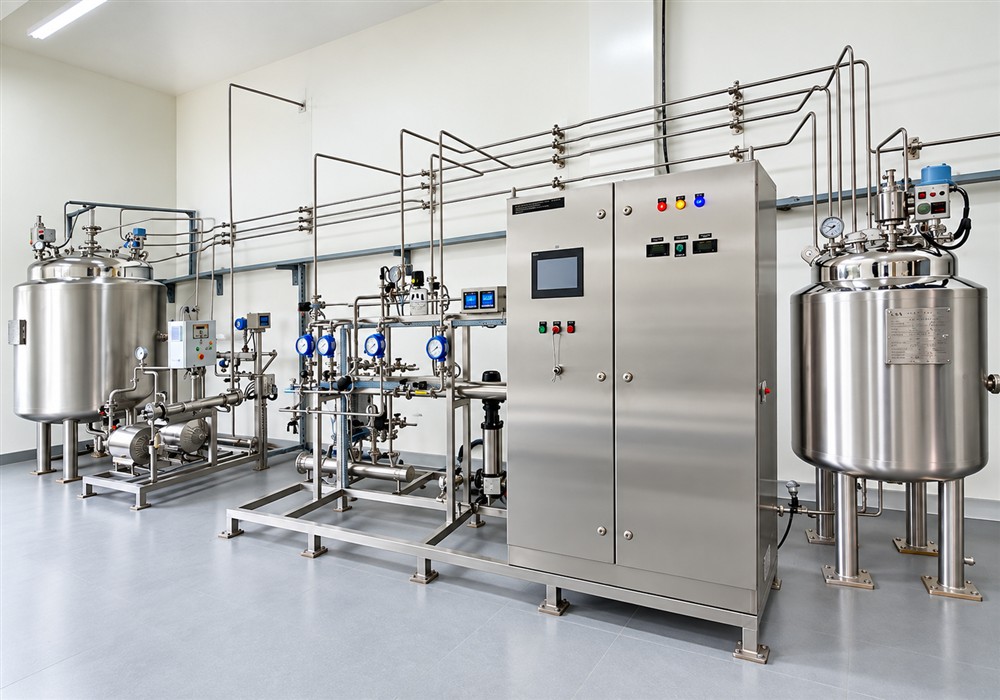
Pilot plant facilities support process trials, scale-up studies and evaluation before moving products into larger production.
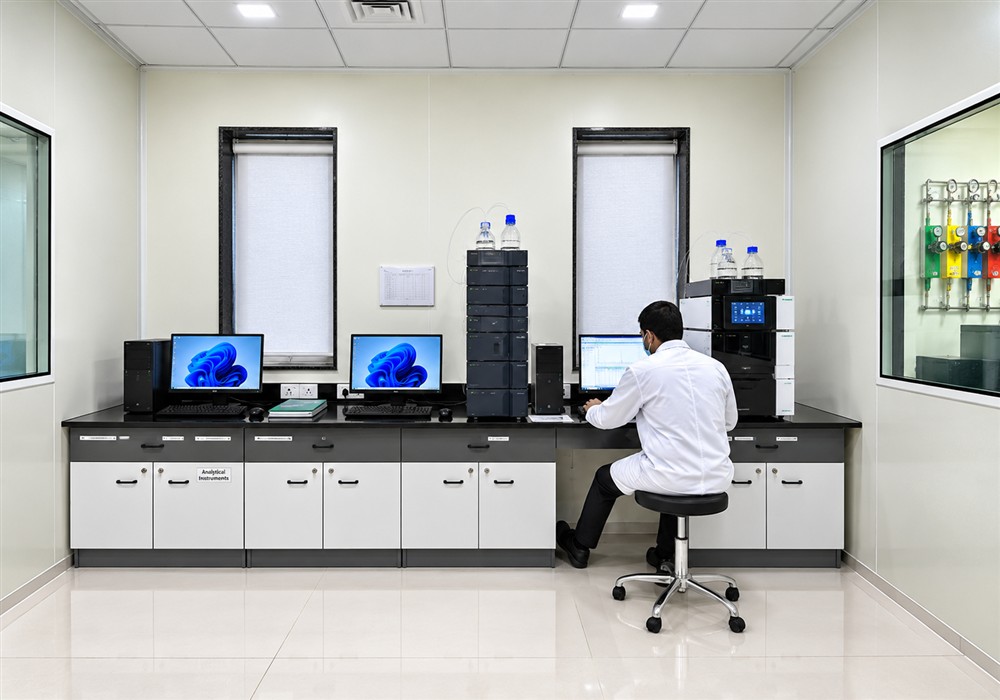
Dedicated R&D facilities support process development, product improvement and scale-up studies for pharmaceutical ingredients.
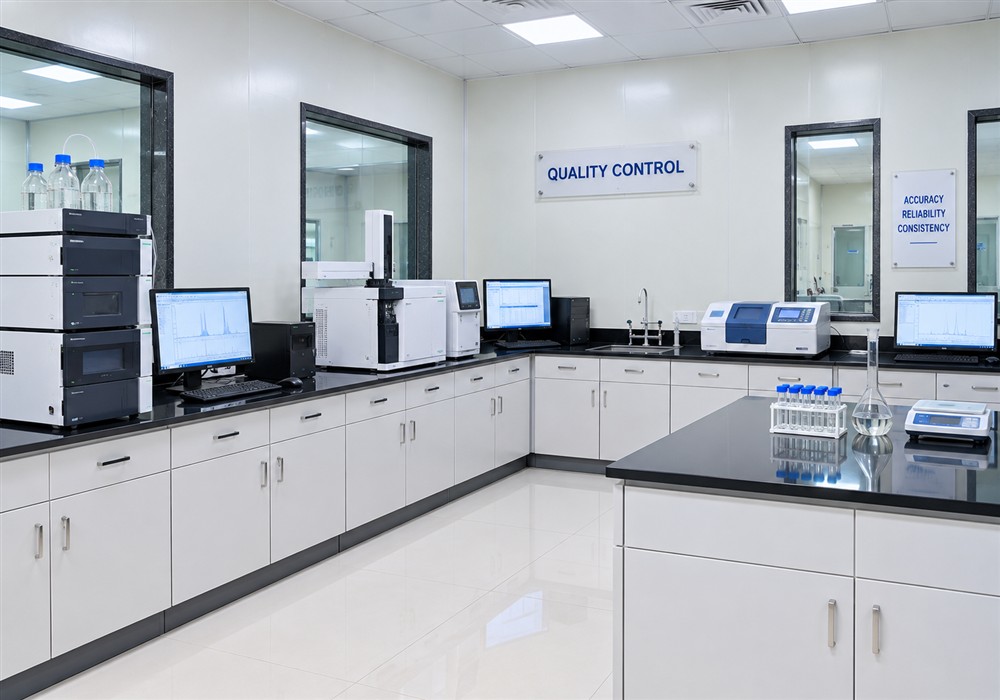
Quality control facilities support analytical testing of raw materials, in-process samples and finished API ingredients.
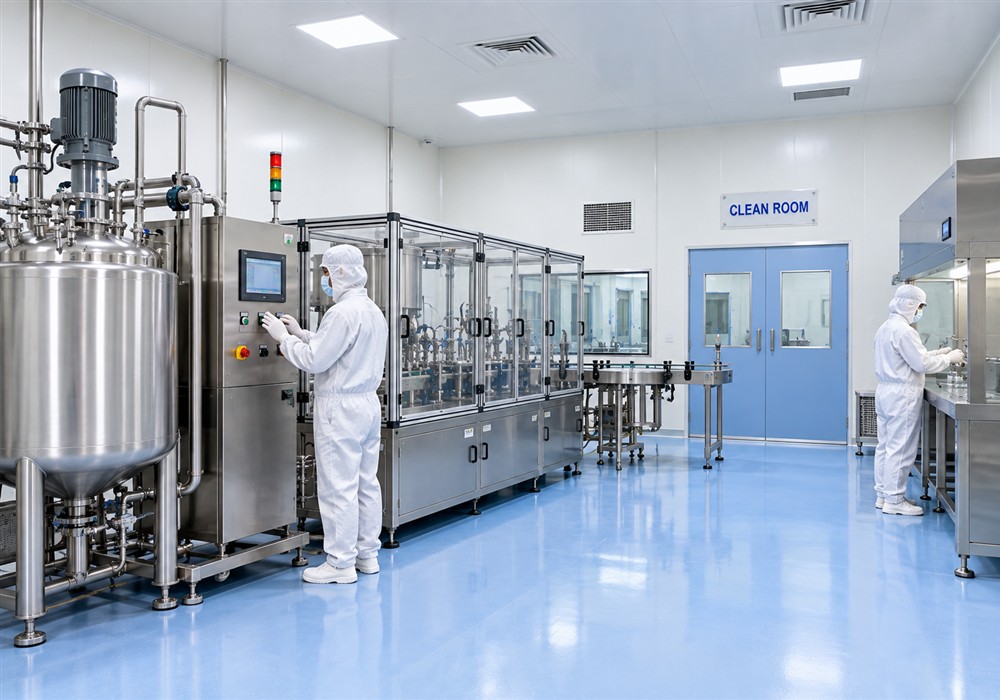
Controlled clean room areas provide suitable environments for API processing, with defined hygiene and operating conditions.
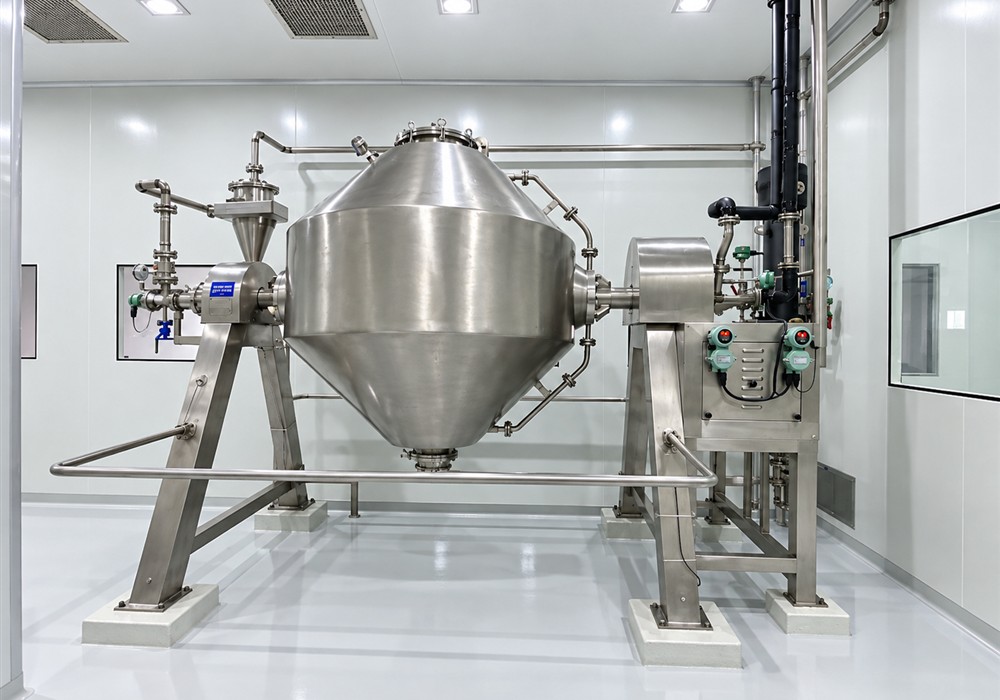
Process and drying equipment supports product handling, moisture removal and controlled steps during API manufacturing operations.
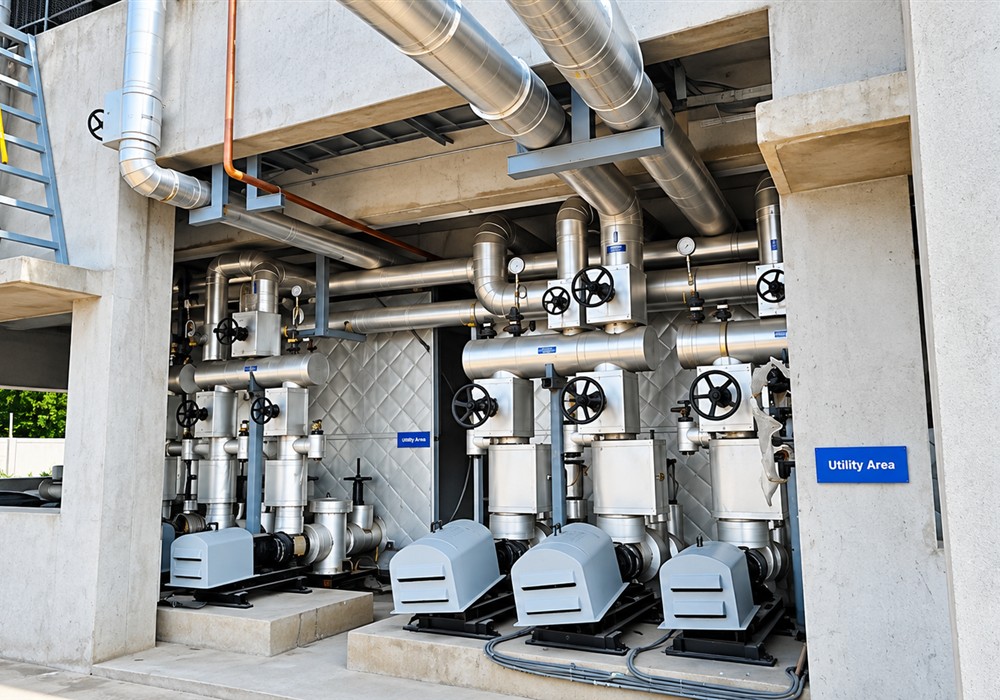
Utility systems support manufacturing operations through organized services, equipment and plant support infrastructure.
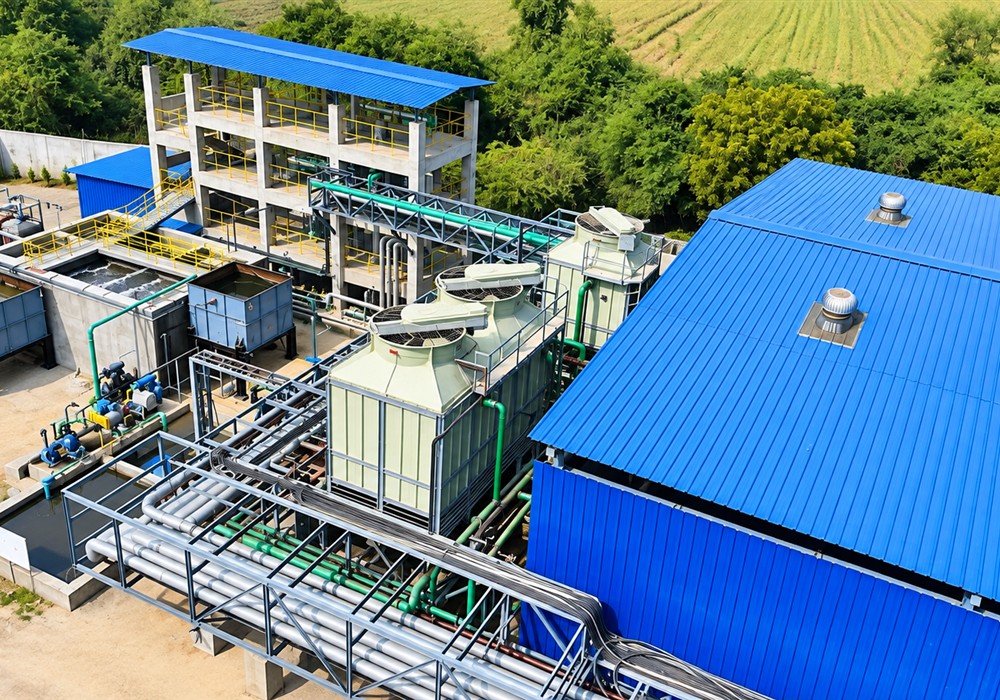
Effluent treatment facilities support handling and treatment of wastewater generated through plant manufacturing activities.
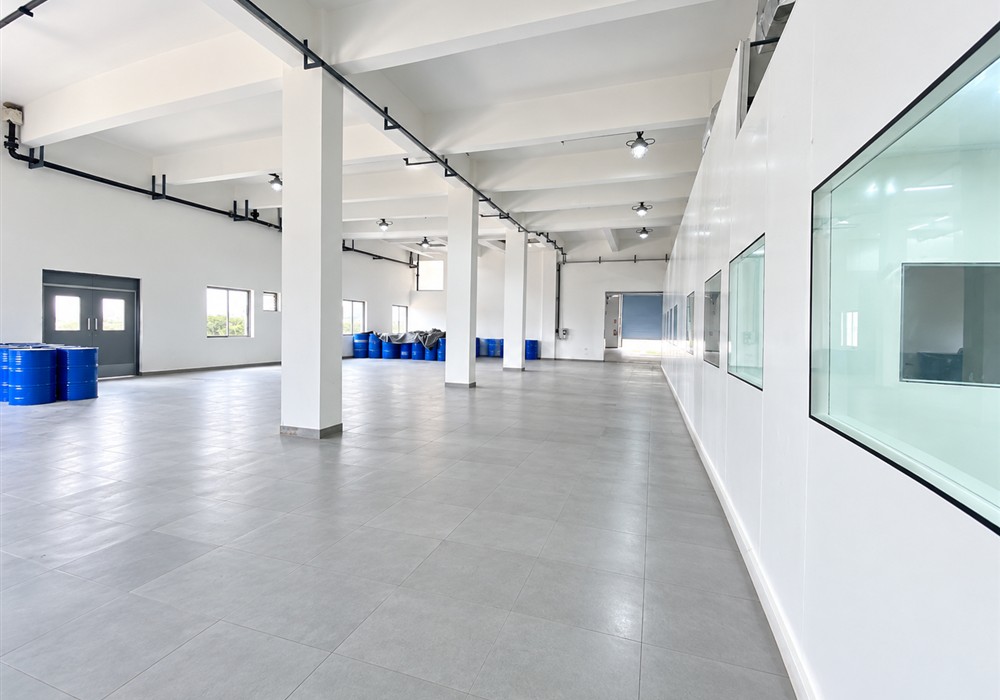
Warehouse and plant infrastructure provides space for material handling, storage, movement and daily supporting operations.
Every certificate we hold reflects how we think, work, and deliver. From quality to safety and sustainability, our processes are audited, approved, and alignedwith the highest global expectations.
Certificates - USFDA, PMDA, ISO 9001/14001/45001, SA 8000, Kosher, Halal, and 21 CFR Part 11 compliance.
Certified quality management system ensuring consistent standards and reliable processes.
Good Laboratory Practices supporting accurate, reliable and consistent laboratory operations.
Good Manufacturing Practices ensuring quality, safety and consistency in every product.
Halal certified products meeting defined quality and compliance requirements.
We reduce our environmental impact through responsible resource use, efficient processes and proper waste management across our manufacturing operations.
We value our people and communities by promoting a safe workplace, responsible practices and positive relationships with employees and the wider community.
We follow defined systems, ethical practices and applicable industry requirements to maintain transparency, accountability and responsible business operations.
Stay updated with Livmore Life Sciences Pvt. Ltd.’s latest developments, industry events, exhibitions and company activities as we continue to expand our presence in the pharmaceutical industry.
Advancing Healthcare Through
Science & Innovation
Survey No. 424, 431, Nana Fofaliya Road,
Vill. Ganpatpura, Karjan, Vadodara - 391210 (Guj.-Ind)